

Description
Synthetic Machining Coolant for Flywheel & Surface Grinding
Key Product Features:
- EXTENDS GRINDING WHEEL LIFE: Designed specifically for flywheel resurfacing and precision grinding operations. Reduces wheel loading and glazing so wheels cut cleaner longer, reducing the need for redressing and wheel replacement costs.
- ECONOMICAL CONCENTRATE: Easily mixes with water at a recommended 5-10% concentration. Mix at 1 part coolant to between 9 and 19 parts water for dilution range. Start more concentrated and dilute as needed for your application.
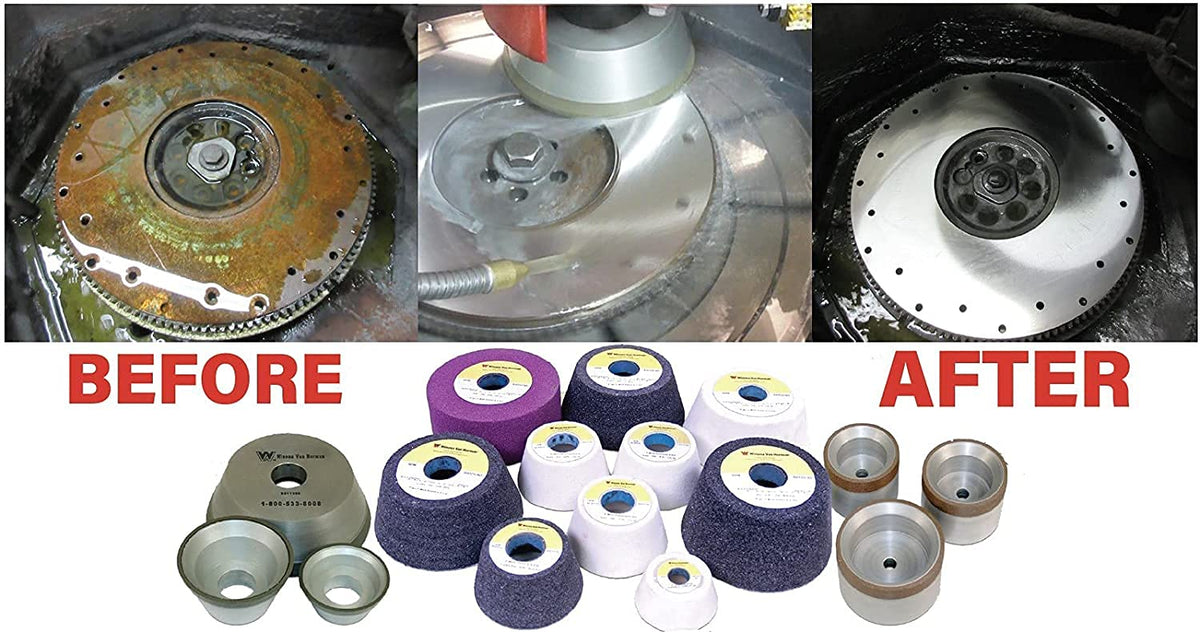
- CONSISTENT SURFACE FINISH: Delivers the flat, consistent finish flywheels need for proper clutch seating. Reduces chatter after resurfacing.
- CLEANER PARTS, CLEANER SUMP: Minimizes residue buildup on workpieces and keeps coolant tanks cleaner, reducing filter changes, sump maintenance, and shop odors associated with prolonged grinding operations.
- FAMILY BUSINESS IN THE HEARTLAND: Winona Van Norman is a family-owned and operated machine manufacturer in Wichita, Kansas, bringing generations of quality engineering to every product we make.
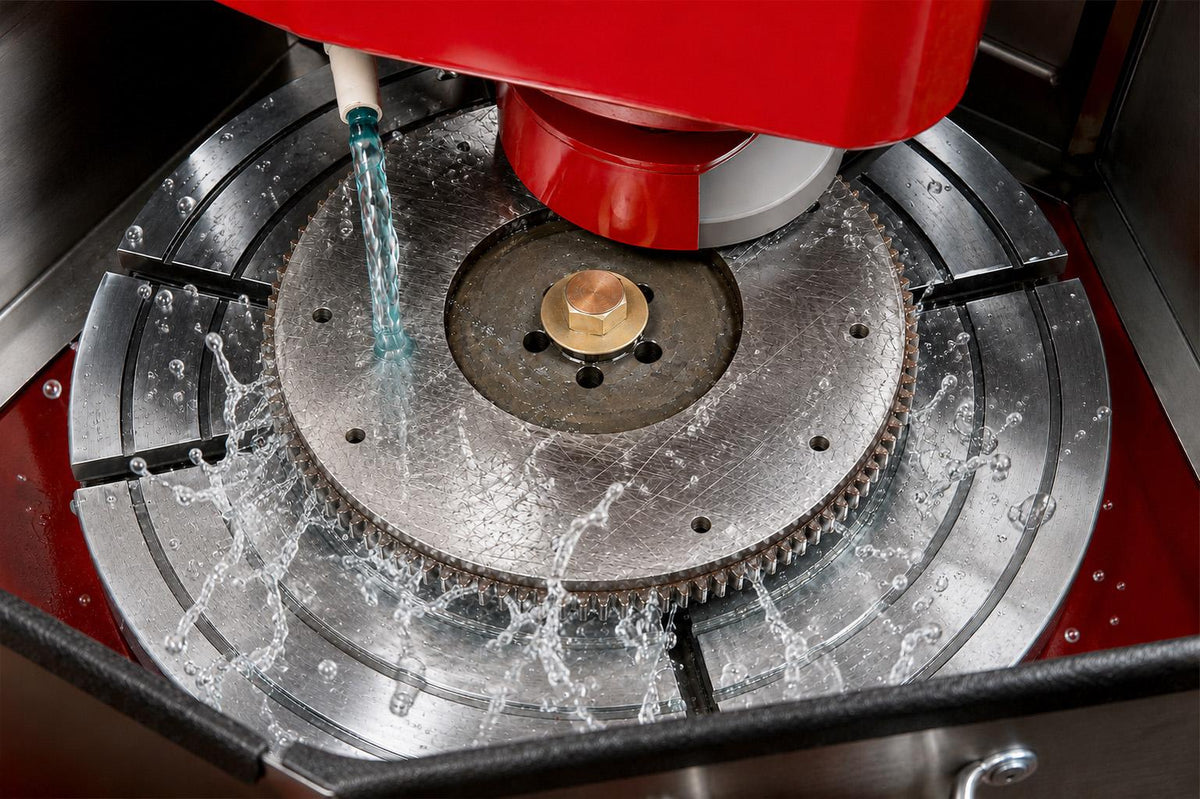
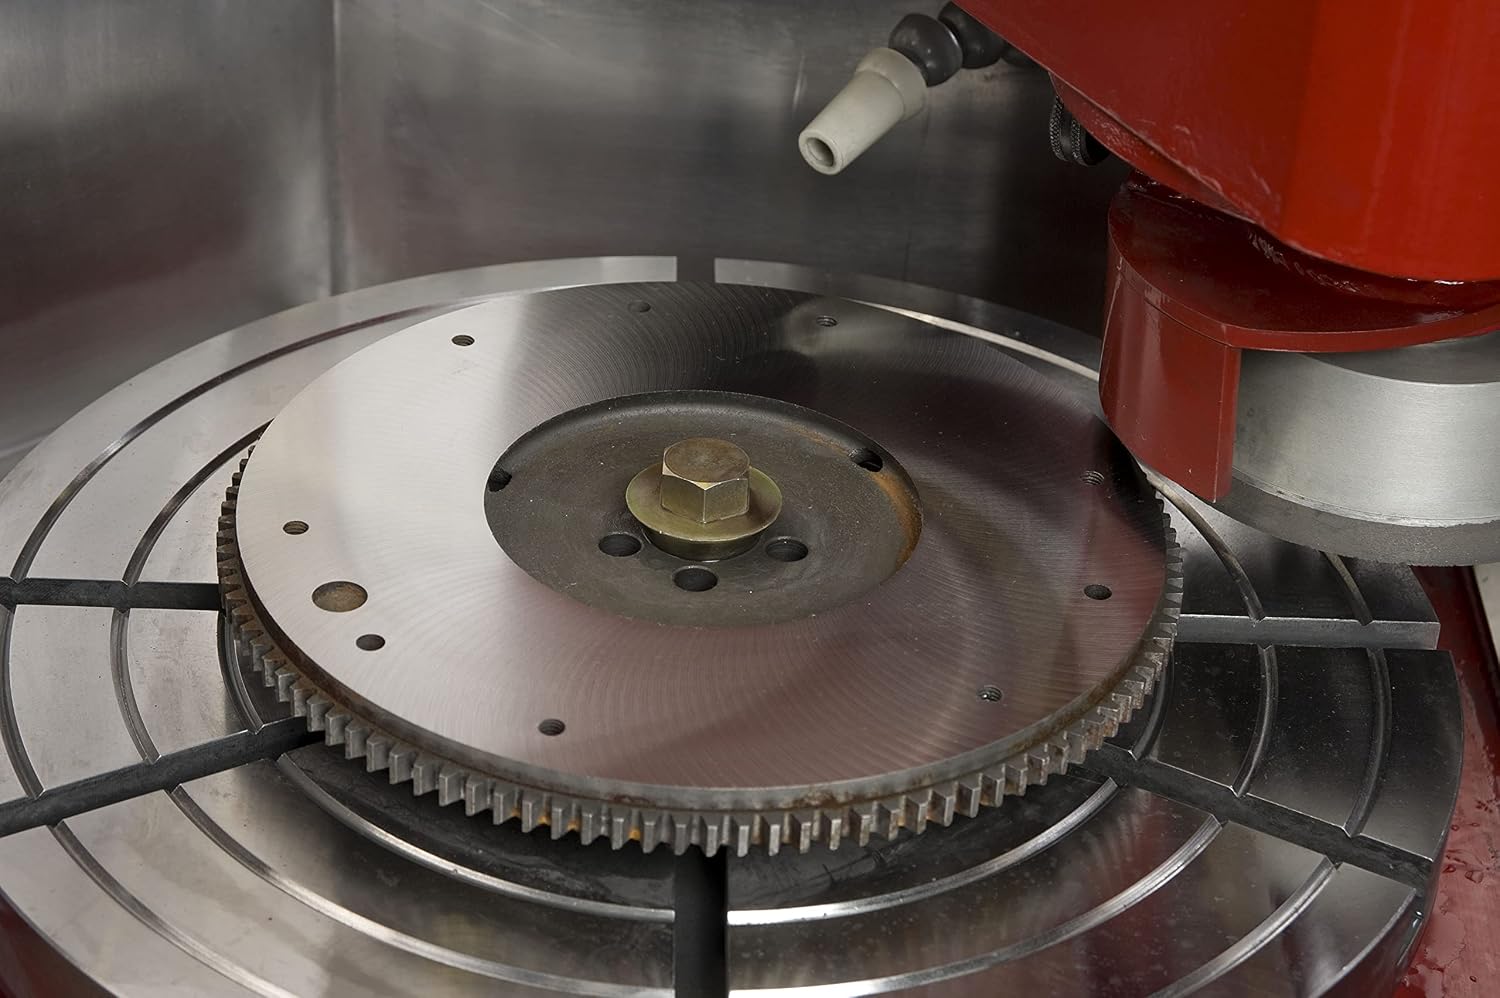
Flywheel grinding puts unforgiving demands on a coolant. The wheel is loading against cast iron and steel across a wide, flat surface, heat builds fast, and any residue left behind shows up as a scratched or hazy finish that fails inspection. Winona Van Norman built this coolant specifically to solve that problem — not as a generic all-purpose fluid stretched to cover grinding, but as a dedicated formula developed in-house for flywheel and precision grinding work. This ultra-concentrated coolant mixes at a minimum of 5–7% with water (roughly 1 part coolant to 20 parts water), so a 5-gallon container goes a long way in the shop. The concentration keeps the grinding wheel cutting cleanly rather than glazing over, which extends wheel life and cuts down on redressing. Parts come off the grinder with a noticeably cleaner, more consistent surface finish, and the coolant itself stays cleaner in the sump — less sludge, less filter changing, less downtime. Machinists and racing teams who run flywheel grinders daily know that coolant choice affects more than just the finish — it affects wheel wear, cycle time, and how often the machine needs attention. A worn or glazed flywheel surface can lead to clutch chatter, uneven engagement, and premature wear on new clutch components, so getting a true, clean regrind matters. This coolant is formulated to help achieve that flat, properly finished surface that a rebuilt or resurfaced flywheel needs to seat correctly. It's also low odor, which matters in shops running grinders for hours at a stretch, and it mixes easily without clumping or requiring special equipment. This is a trusted, shop-tested recipe from a Midwest family business, made and tested in the USA — the same coolant formula used in Winona Van Norman's own machine shop. Mixing instructions: Combine 1 part coolant to 20 parts water for a 5% concentration (minimum recommended). Adjust ratio up for heavier grinding applications as needed.